Glare and low contrast
Highly reflective or dark surfaces may need controlled illumination geometry to reveal cell boundaries.
Read and assess laser-marked, dot-peened and etched Data Matrix codes on metal, plastic and other industrial parts under controlled production conditions.
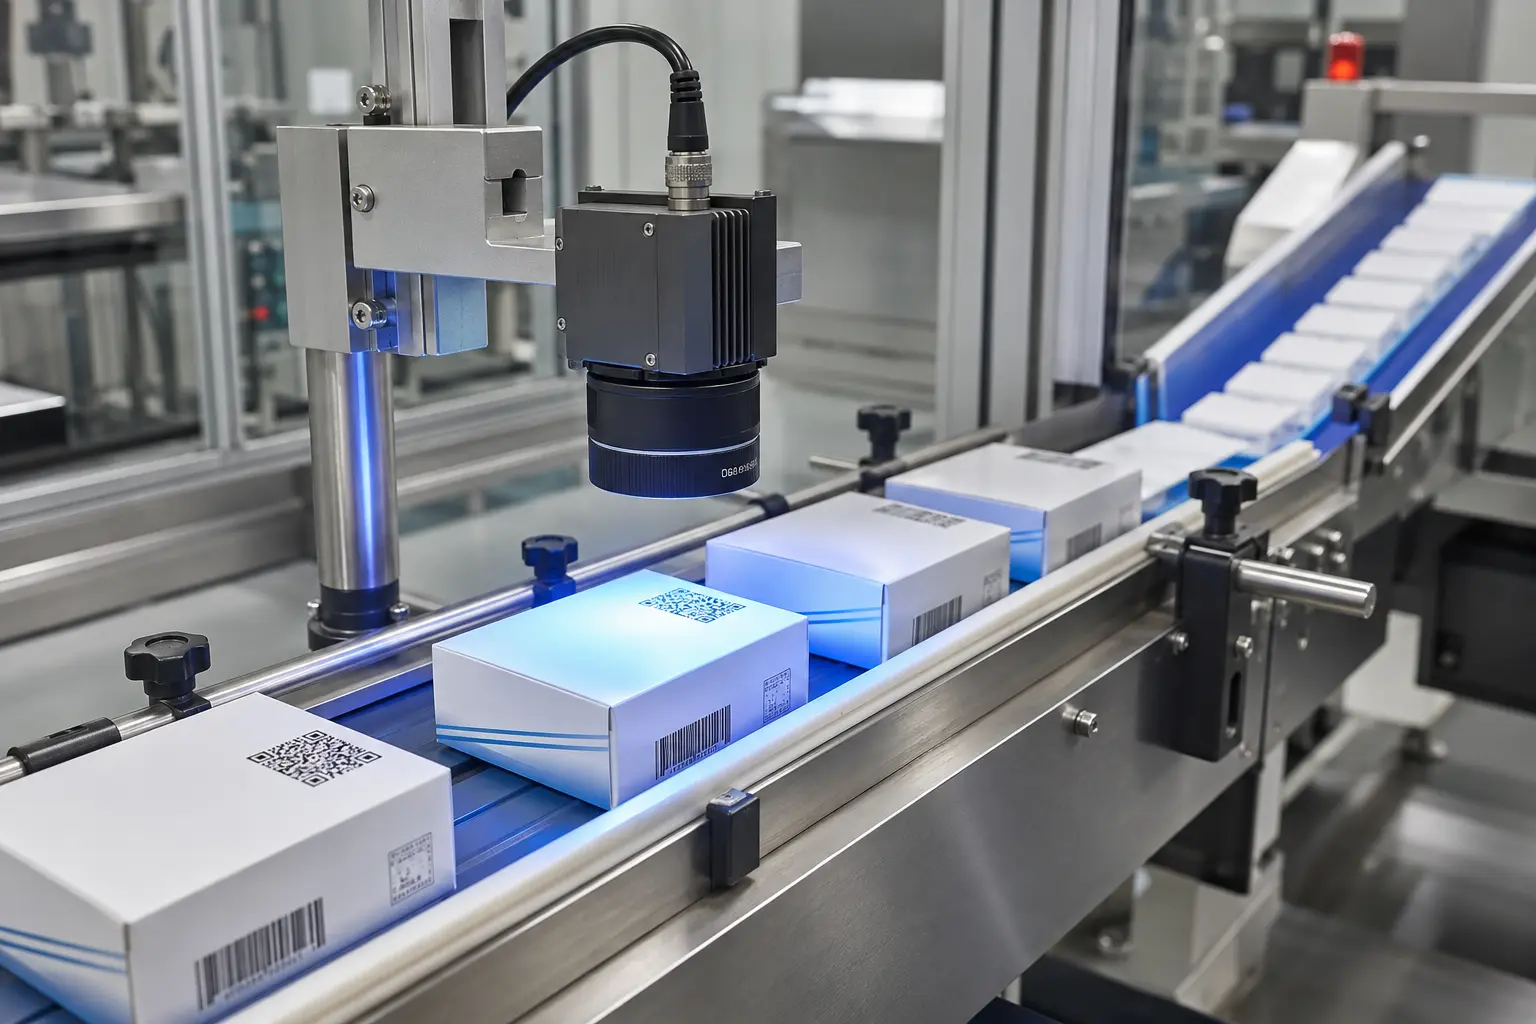
DPM Data Matrix verification needs imaging and illumination designed for the marked surface. ISO/IEC 29158:2025 adapts the two-dimensional quality method for direct part marks and defines alternative lighting and reporting conditions.
Laser annealing, laser engraving, dot peen and chemical etching produce very different cell shapes and reflectance. Machining marks, coatings, curvature and oil can further change the image as the part rotates or moves.
A production project should therefore test the worst credible surfaces and mark positions, not only a perfect sample. Where formal grading is required, the applicable illumination and calibration method must be stated; where the goal is reliable production reading, the acceptance test should still define realistic limits.
Highly reflective or dark surfaces may need controlled illumination geometry to reveal cell boundaries.
Code position, working distance and part rotation can alter module shape and apparent quiet zones.
Shallow dots, over-marking, debris and process drift can reduce decoding and quality margin.
Exposure time, trigger accuracy and fixture repeatability determine the captured production image.
Primary reference: ISO/IEC 29158:2025 — direct part mark symbol quality test specification.
We can trial lighting, resolution, reading margin and data checks before final system hardware is selected.
Technical content reviewed by the Oxford Vision Systems engineering team. Updated 26 August 2026.
Concise answers to the questions manufacturers ask when defining a barcode inspection application.
Ask an engineerIt is a two-dimensional code marked directly onto a component rather than printed on a separate label. Common marking methods include laser, dot peen and chemical etching.
Direct marks may have low or uneven contrast, specular reflections, surface texture, curved geometry or incomplete cells. The reader, lens and illumination must be selected for the actual surface and mark.
ISO/IEC 29158:2025 defines modifications to the ISO/IEC 15415 symbol-quality methodology for direct part marks, including alternative illumination conditions and reporting requirements.
Often yes, but the smallest module, motion, orientation, working distance, surface finish and required grade must be proven with representative parts at realistic handling conditions.