Automatic reject integration
Remove every failed code with a reject system designed for the product
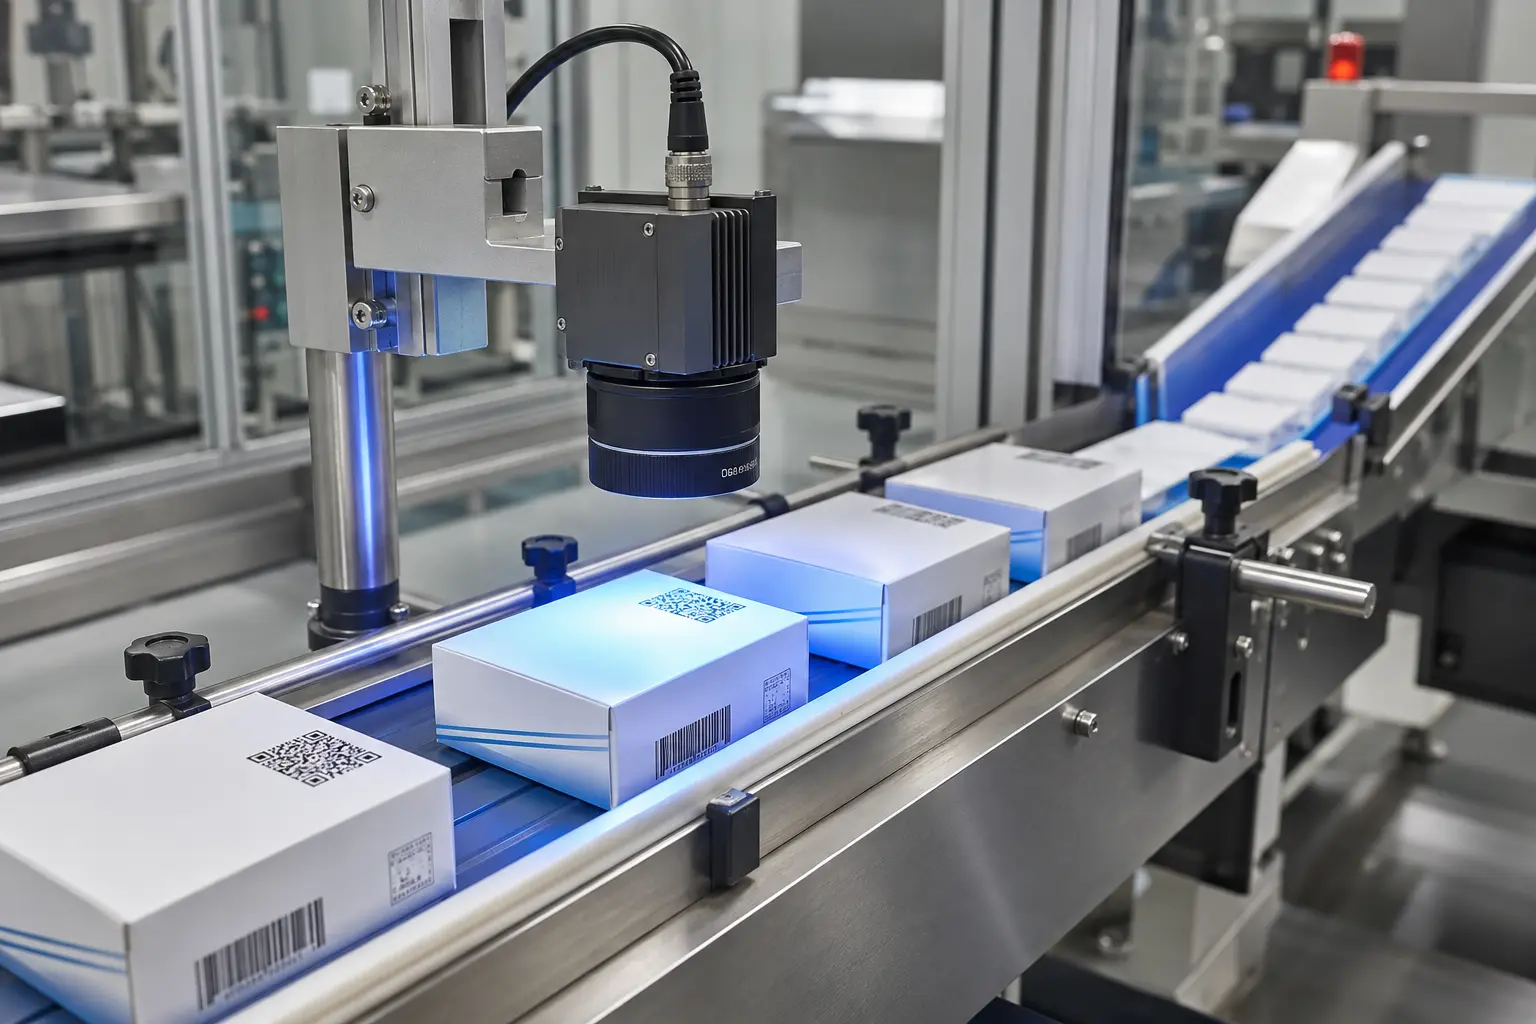
Inspection only protects your customer when failed product is physically controlled. We integrate the vision decision with a suitable reject mechanism, confirm the reject event and provide a clear response if the product is not removed as expected.
Application focus
Close the loop between detection and containment
Reject choice depends on product weight, stability, speed, spacing, line layout and the type of failure. Options include air blast, pusher, sweep arm, drop flap, retracting conveyor, stop gate and diverter. A dedicated reject bin can include level monitoring, access control and removal detection.
Product tracking maintains the link between the camera result and the correct item as it travels to the reject point. Sensor confirmation and encoder tracking can be used to detect missing products, late rejects or unexpected items in the reject path.
Designed around the risk
What the system helps you achieve
Verify physical removal
Prevent reject-bin tampering
Stop on abnormal reject events
A proven project route
From sample to a production-ready inspection
We define the pass criteria first, prove the imaging and data logic, then integrate the complete inspection and reject sequence.
Application review
Product, code, substrate, speed, line layout and data requirements.
Sample trials
Optics, lighting, resolution and achievable tolerance tested on real packs.
System integration
Camera, controls, guarding, reject and upstream interfaces engineered together.
Commissioning
Recipes, fault handling, training and agreed acceptance tests completed.
Common questions
What manufacturers ask us
Every line is different. These are the practical questions that shape a dependable barcode verification project.
Ask an engineerWhich reject method is best?+
It depends on the pack, speed and available space. We select and trial the mechanism after reviewing product stability, weight and acceptable handling.
How does reject confirmation work?+
A downstream sensor confirms the targeted pack entered the reject path. If confirmation is absent, the system can alarm and stop the line.
Can good and failed products be tracked close together?+
Yes, subject to minimum spacing and sensor control. Encoder tracking maintains the inspection result against the physical product through the reject sequence.
Oxford Vision Systems
Let’s prove the inspection on your product
Share samples, code specifications and target line speed for an initial application review.